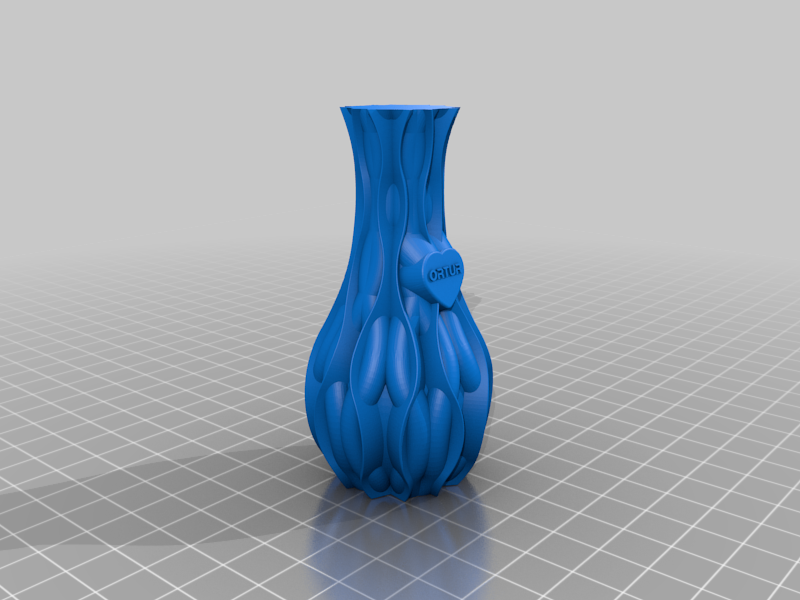
Its My GCODE what i use.
Mein GCODE was is so nutze.
------------Start Code-----------------------
G21 ; set units to millimeters
G90 ; use absolute positioning
M82 ; absolute extrusion mode
M104 S{material_print_temperature_layer_0} ; set extruder temp
M140 S{material_bed_temperature_layer_0} ; set bed temp
M190 S{material_bed_temperature_layer_0} ; wait for bed temp
M109 S{material_print_temperature_layer_0} ; wait for extruder temp
G28 X0 Y0 ;move X/Y to min endstops
G28 Z0 ;move Z to min endstops
;G29 ;auto level
G0 X0 Y15 F9000 ; Go to front
G0 Z0.15 ; Drop to bed
G92 E0 ; zero the extruded length
G1 X40 E25 F500 ; Extrude 25mm of filament in a 4cm line
G92 E0 ; zero the extruded length
G1 E-1 F500 ; Retract a little
G1 X80 F4000 ; Quickly wipe away from the filament line
G1 Z0.3 ; Raise and begin printing.
--------------------EndCode-------------------------
M104 S0 ; turn off extruder
M140 S0 ; turn off heatbed
M107 ; turn off fan
G91 ; relative positioning
G1 Z25 ; raise head 25mm
G90 ; back to absolute positioning
G1 X0 Y220; home X axis and push Y forward
M84 ; disable motors
Category: 3D Printing
Ortur Obsidian - GCODE
by ErroXCoder · original on Printables ↗
Hobby & Makers / Other Ideas
♥ 7⬇ 1.9k🖨 0 prints
Print profiles
Ortur_Vase_1.stlDEFAULT
⏱ time and weight estimated after preparation · 1 material(s)
Made to order: we prepare this file when you order, which adds a few minutes before printing starts.
Prints on: A1 mini 0.4PLA
Order this print